Quality & Food Safety for Food & Beverage
Consistent quality protects your consumers and your brand. We build practical quality and food safety systems that shop-floor teams can follow every shift.
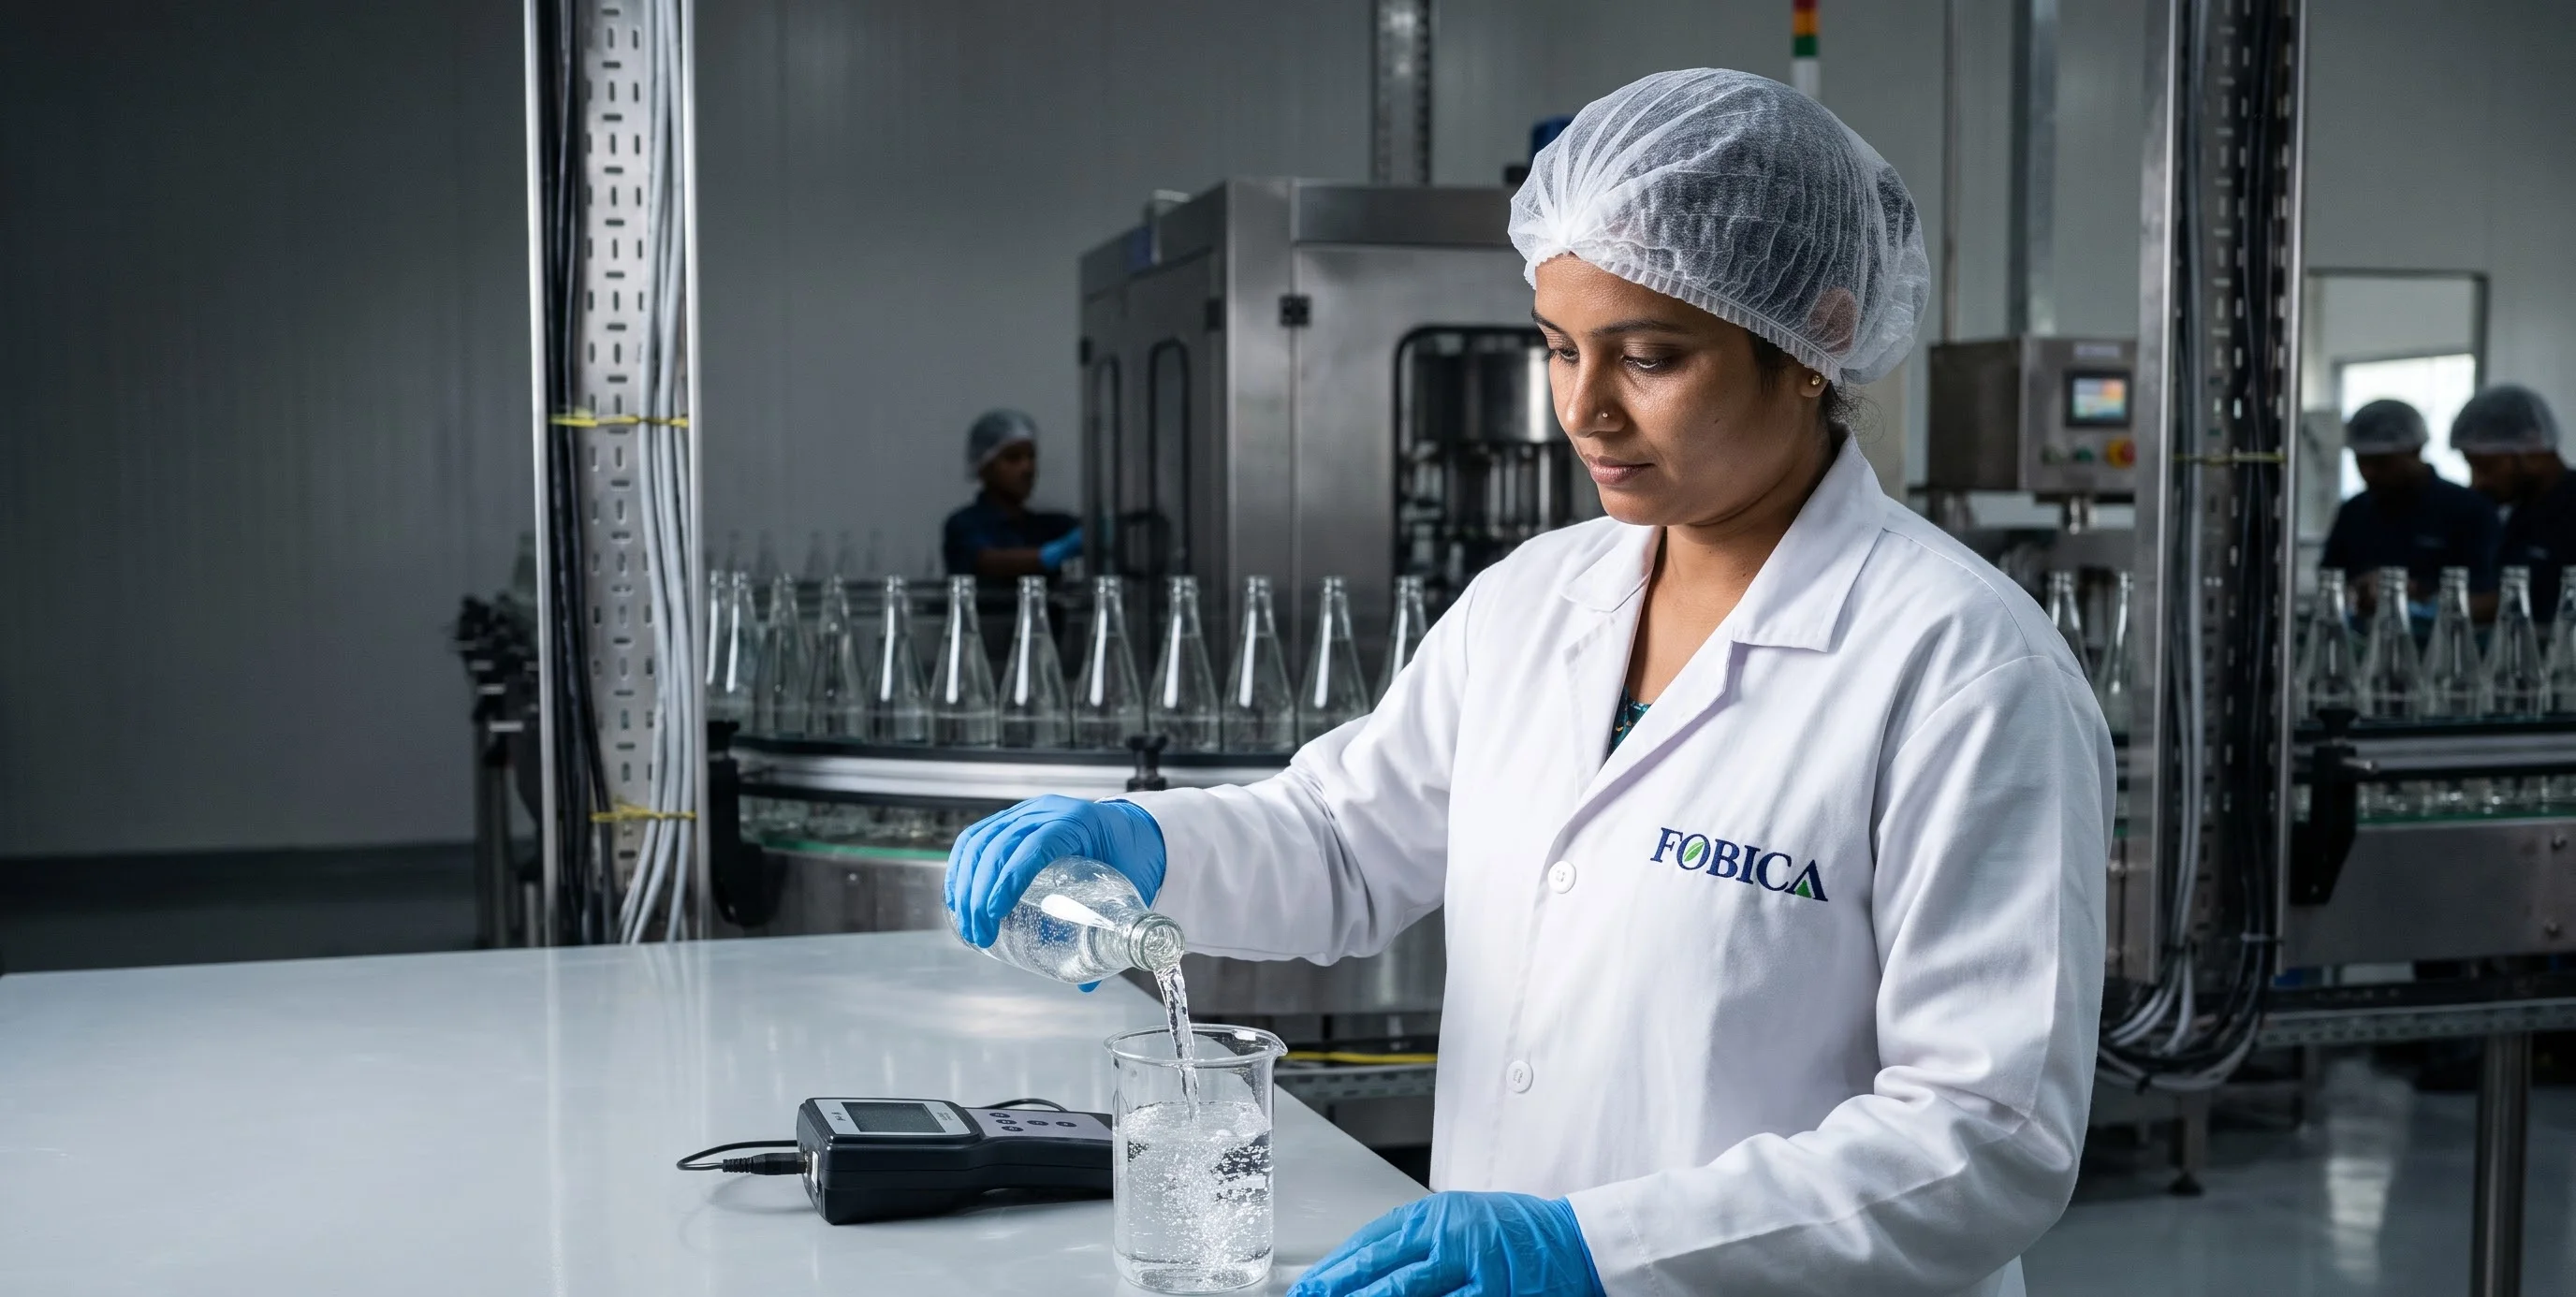
Quality your teams can run
Quality comes from the specifications, checks, records and habits that make every batch the same. We design them around your product, your line and your people.
From a QC laboratory that matches your testing scope to SOPs operators follow on a busy shift, the system is built to hold up during audits and on ordinary days.
Problems we solve
- Inconsistent quality from batch to batch
- SOPs that nobody follows
- A laboratory that cannot test what it needs to
- Unclear specifications for materials and products
- Stressful, last-minute audit preparation
Nine parts of a quality system
Quality management systems
A structured framework of policies, procedures, records and reviews.
SOP development
Clear, practical standard operating procedures for every critical activity.
QC laboratory planning
Laboratory layout, equipment, testing scope and staffing for in-house quality control.
Raw material specifications
Clear acceptance criteria for incoming materials and packaging.
Finished product specifications
Defined quality parameters for every product and pack.
Quality-control systems
In-process checks, sampling plans and product release procedures.
Food safety systems
Hazard-based food safety controls, hygiene, sanitation and traceability.
Audit preparation
Readiness for regulatory, customer and certification audits.
Process improvement
Fix the root causes of quality problems and reduce variation.
Built for four kinds of client
Entrepreneurs
Building a first plant that must be right-sized and compliant.
Existing manufacturers
Adding lines, capacity or a second site.
Brand owners
Moving from co-packing to their own manufacturing.
Corporates
Need specialist project or operational support.
Concentrated in Plan and Implement and Optimise
- Understand
- Analyse
- Plan
- Implement
- Optimise
- Grow
Typical deliverables
- Quality manual and policies
- SOP and work instruction set
- QC laboratory plan and equipment list
- Material and product specifications
- Sampling and release procedures
- Audit readiness checklist
Quality questions
Do we need an in-house QC laboratory?
Many plants do, and some products require specific testing. We plan the scope, equipment and people to match.
Can you help us pass a customer audit?
Yes. We review your systems against the audit scope and close the gaps before the auditor arrives.
How do you make SOPs stick?
We write them with the people who use them, keep them short and visual, and train supervisors to check them.
Can you fix recurring quality problems?
Yes. Process improvement finds the root cause rather than adding more inspection.
Quality problems you want solved for good?
Tell us about your product, line and the issues you see. We will suggest where to start.